How to Set Cosmetic Quality Limits for Custom Headphones
Sort the defects into three bands
Appearance is not one thing. A visible scratch on the earcup side and a faint mark inside the headband are different problems, and they deserve different limits. The first step in acceptance is to sort them: which defects get zero tolerance, which allow a small count, and which pass without action.
Then set an allowed count for each band. Inspection is sampling, so nobody looks at every unit in detail. How many units to pull and how many defects to allow needs a written rule. The ISO 2859-1 standard defines sampling schemes built on the acceptance quality limit, which is the average share of defective units a buyer agrees to accept in a lot. Lot size, sample size, and acceptance number all come from a table. Your acceptance document does not need the whole standard. Take the structure of bands plus allowed counts.
Write the color difference as a number
Color is the hardest dispute to settle, because the human eye follows the light. The same headset looks like one color in daylight, another under warehouse lighting, and two people can see a third.
The answer is a number. A spectrophotometer measures the color difference as a ΔE value, one figure that states how far two batches sit apart. Konica Minolta's technical note gives the working thresholds: below 1 the eye cannot tell, 1 to 2 shows up only under close inspection, and above 3 the difference is clear and most industries reject it.
Three items go into your standard: the ΔE limit, the light source used for measurement, and which part of the product gets measured. Where you set the limit depends on your product positioning. Confirm the factory owns a spectrophotometer before you write it, or the standard stays empty.
Write the scratch limit as a viewing condition
No obvious scratches on the surface cannot be executed. How small is small, and how bright the light has to be before a mark counts as visible, have no answers.
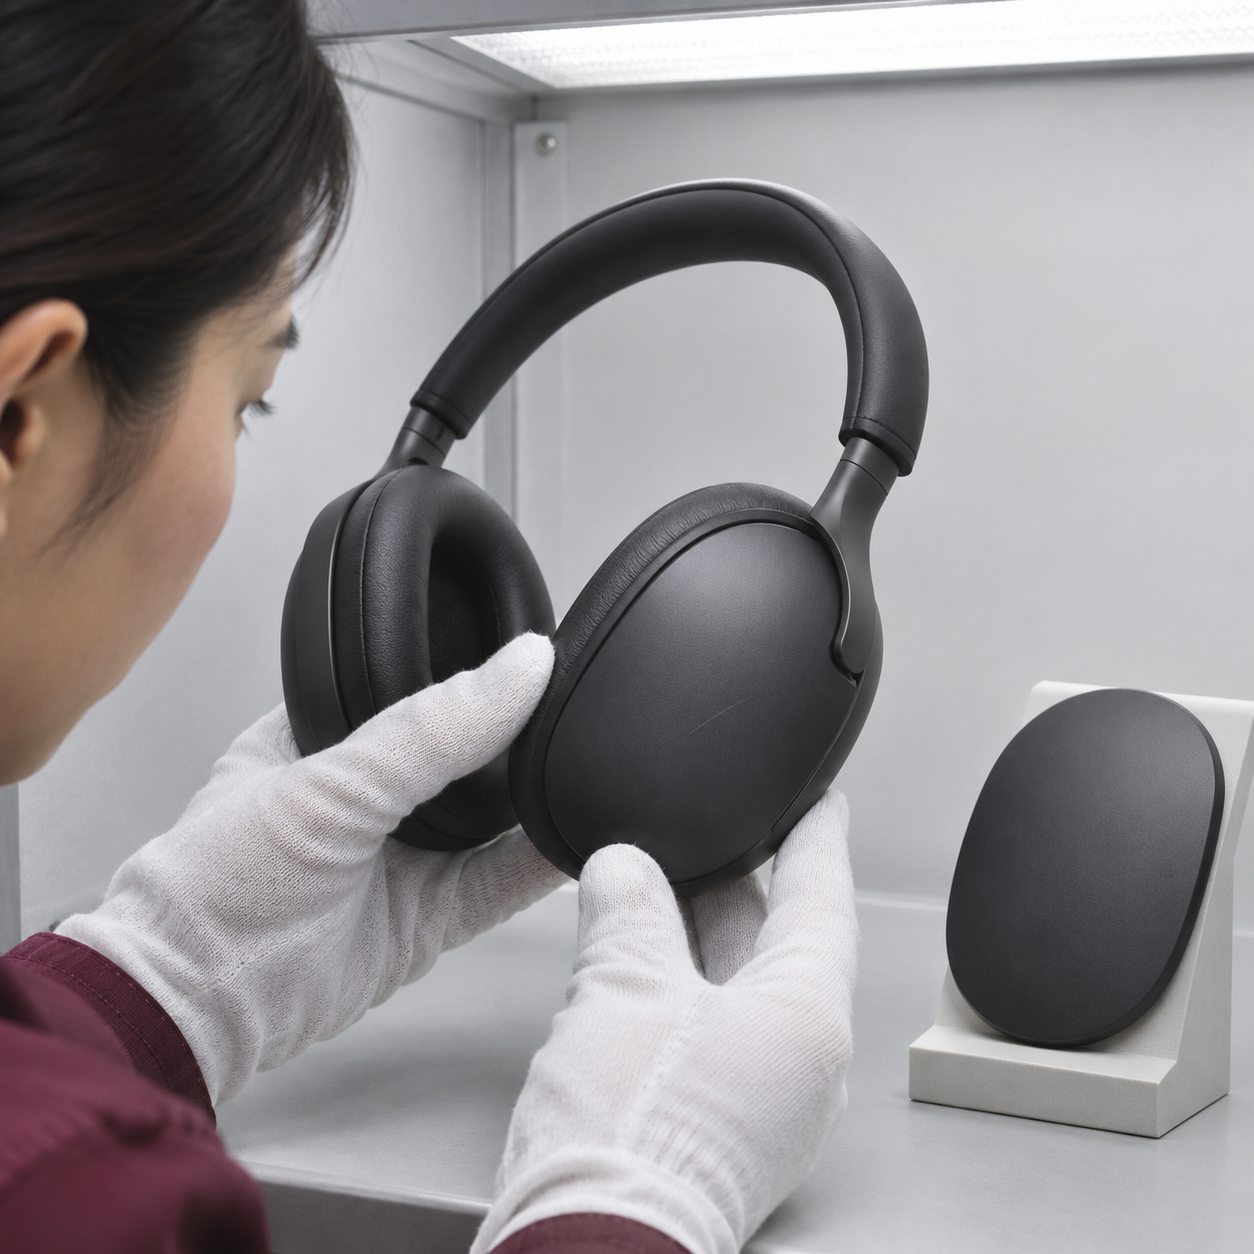
The workable version fixes the viewing condition: how bright the light is, how far the inspector stands, how long they look, and from which angle. Once the condition is written down, the word visible has a boundary. A scratch nobody can see under those conditions passes.
The exact values have no single right answer. What matters is that both sides sign them. When the room and the inspector change, the judgment still holds, because the numbers were fixed in advance.
Mark the pass boundary with a physical sample
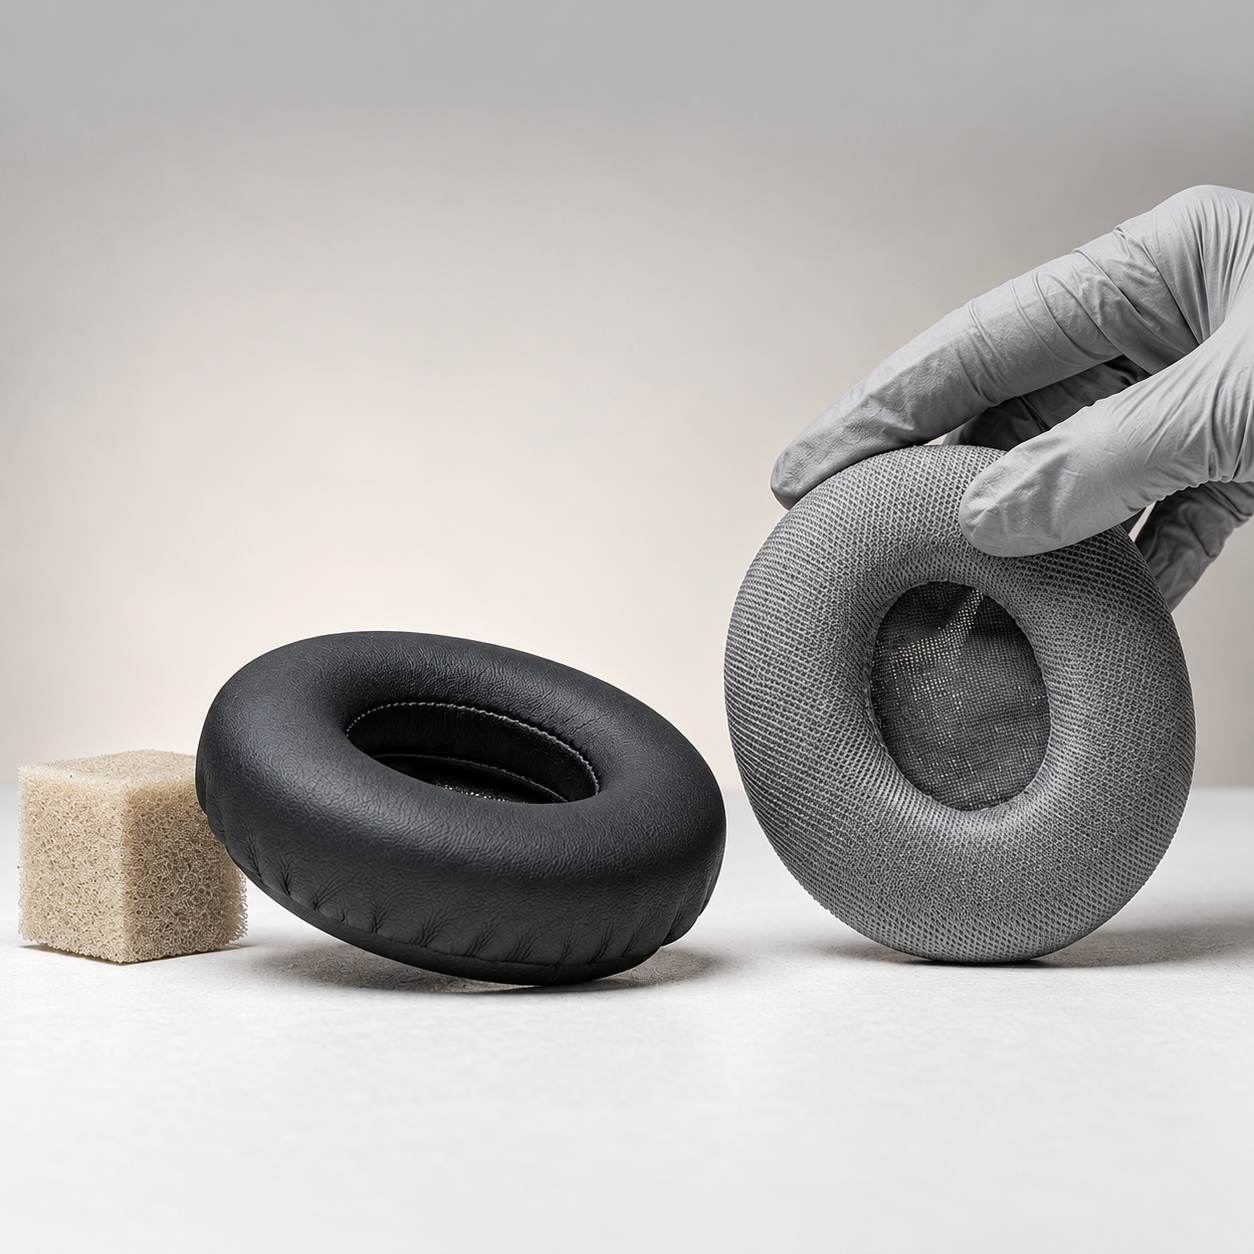
Words cannot describe every boundary, so draw the line with a physical object. Pick the sample whose scratch sits exactly on the acceptance line, have both sides sign it, and keep one copy each. At inspection, a scratch lighter than this sample passes, and a scratch heavier than it fails. This signed sample is the boundary sample. Color works the same way. Seal a standard color chip and let it confirm the ΔE reading.
Seal the boundary samples before mass production starts, not after a problem appears. Once the shipment is finished, picking which unit counts as the boundary starts the argument again.
Write the gaps and the logo too
Appearance is not only the surface. The assembly gap between earcup and headband, and the position and sharpness of the logo, both turn into complaints at the return desk, and most contracts skip them.
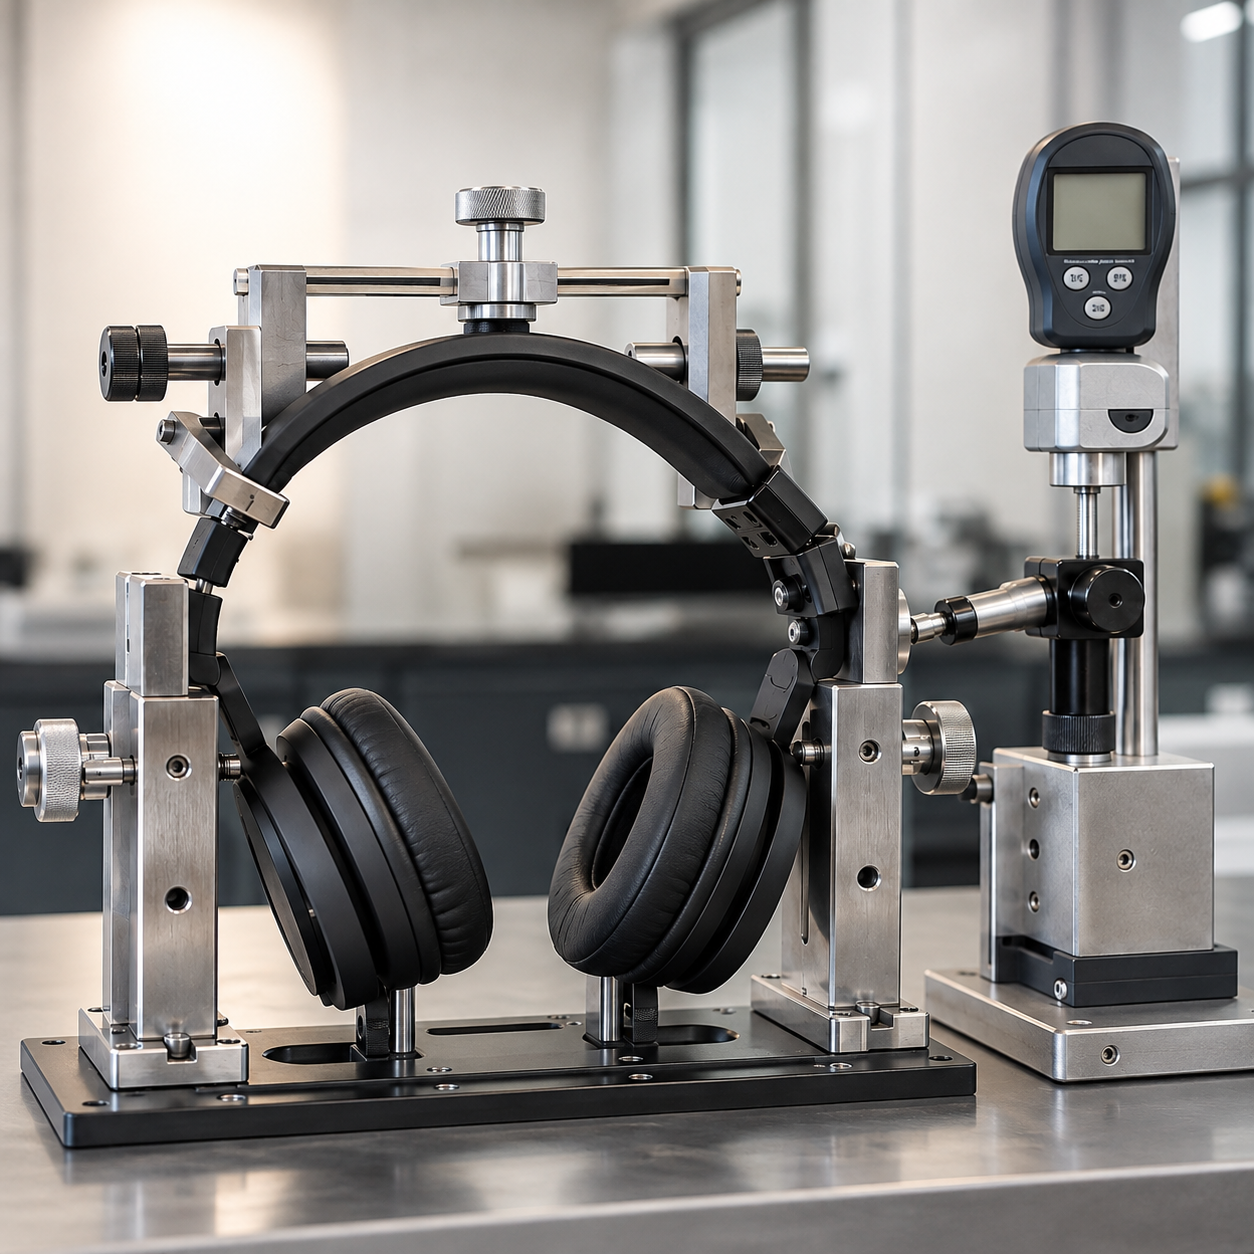
Measure the gaps with a feeler gauge, the set of thin steel blades used to check a gap width, and write the upper limit for each joint. For the logo, state how far it may shift and how sharp the print must stay, with a boundary sample sealed beside it. These items are small and cheap to write. Missing them costs a whole shipment's worth of argument.
Put it all on one acceptance page
Scattered clauses do not get executed. Collect them on one page and send it out with the RFQ and the purchase order.
| Appearance item | How to judge | What the standard must state |
|---|---|---|
| Color | ΔE measured by spectrophotometer | Acceptance limit, light source, measured area |
| Scratches and coating | Visual check under fixed conditions | Illuminance, distance, viewing time, boundary sample ID |
| Assembly gaps | Feeler gauge | Upper gap limit for each joint |
| Logo and print | Visual check against sample | Allowed offset, sharpness boundary sample |
An appearance requirement that never reaches the purchase document does not exist at inspection. Cosmetic limits follow the same logic as comparing two OEM quotes. Agree the measuring basis first, then the comparison means something.
Send Sonun your appearance requirements, your color acceptance limit, and your boundary-sample expectations. We will prepare the boundary samples and the inspection record on that basis and ship them with the samples for your confirmation.